
High-Speed Closure & Cap Architectures
Consumer packaging demands high aesthetic polish, zero parting-line flash, perfect thread engagement, and microscopic living hinges that flex thousands of times without tearing.
Primary Packaging Product Verticals
- Flip-Top Dispensing Caps: Shampoo, lotion, and condiment lids featuring integrated butterfly living hinges and snap spouts.
- Tamper-Evident Beverage Closures: Water and carbonated soft drink closures incorporating mechanical breakaway bands and gas-tight bore seals.
- Dual-Color Dispensing Caps: Multi-shot 2K closures combining a colored body with an elastomeric dispensing valve or soft-touch grip.
- Thin-Wall Deli & Dairy Tubs: Containers molded under 0.50 mm wall thickness with high-acceleration injection and air poppet ejection.
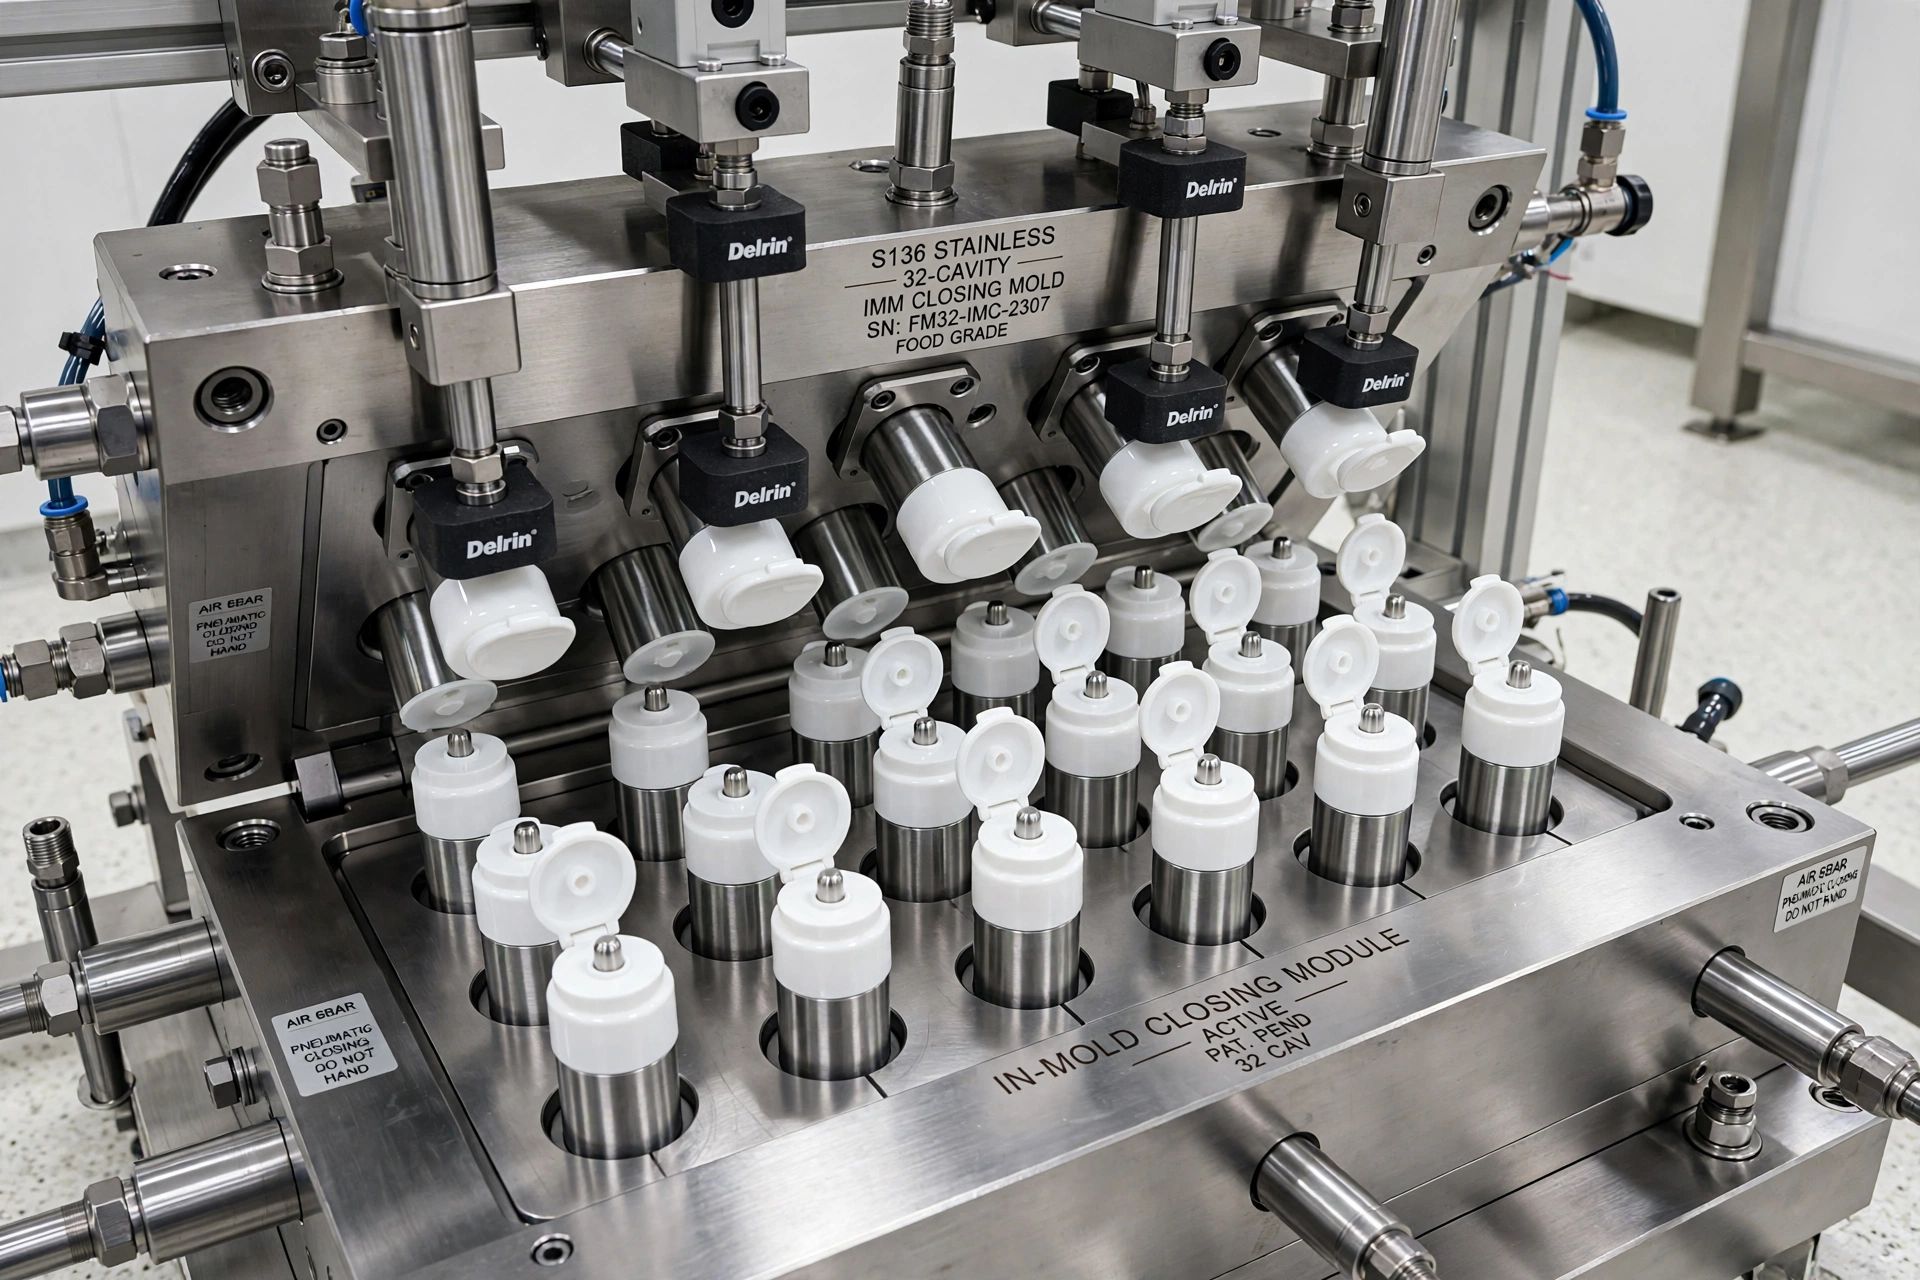
Automated In-Mold Flip-Top Hinge Closing
Closing the flip-top lid inside the mold while the polypropylene polymer chains are still hot and unoriented strengthens the molecular alignment across the living hinge. This eliminates secondary offline capping labor, reduces cleanroom floor clutter, and delivers parts ready for direct bulk cartoning. Explore our high-cavitation and stack mold solutions for packaging.
Precision Rotary Unscrewing Mechanisms
For deep internal bottle cap threads that cannot be mechanically stripped without thread stripping, our toolroom manufactures precision rotary unscrewing molds.

Unscrewing Drive Methods
- Hydraulic Rack and Pinion: Machine ejector stroke or auxiliary hydraulic cylinder drives a geared rack that spins internal core gears simultaneously.
- Servo Electric Drive: Independent high-torque servo motor providing programmable acceleration, deceleration, and thread position indexing.
- Collapsible Cores: Segmented core pins that contract radially inward to release internal threads instantly without rotation, cutting cycle time by two to three seconds.
Thin-Wall Packaging Container Tooling
Extreme Pressure and Acceleration
Molding thin-wall margarine tubs, yogurt cups, and beverage containers with wall thicknesses down to 0.35 mm requires injection velocities exceeding 600 mm/sec and injection pressures up to 2,500 bar.
Our thin-wall tools feature vacuum heat-treated S136 stainless steel inserts, air poppet valves to assist mechanical stripper rings, and zero-deflection interlocking tapered core lock rings. Explore our advanced conformal cooling inserts for rapid container cooling.
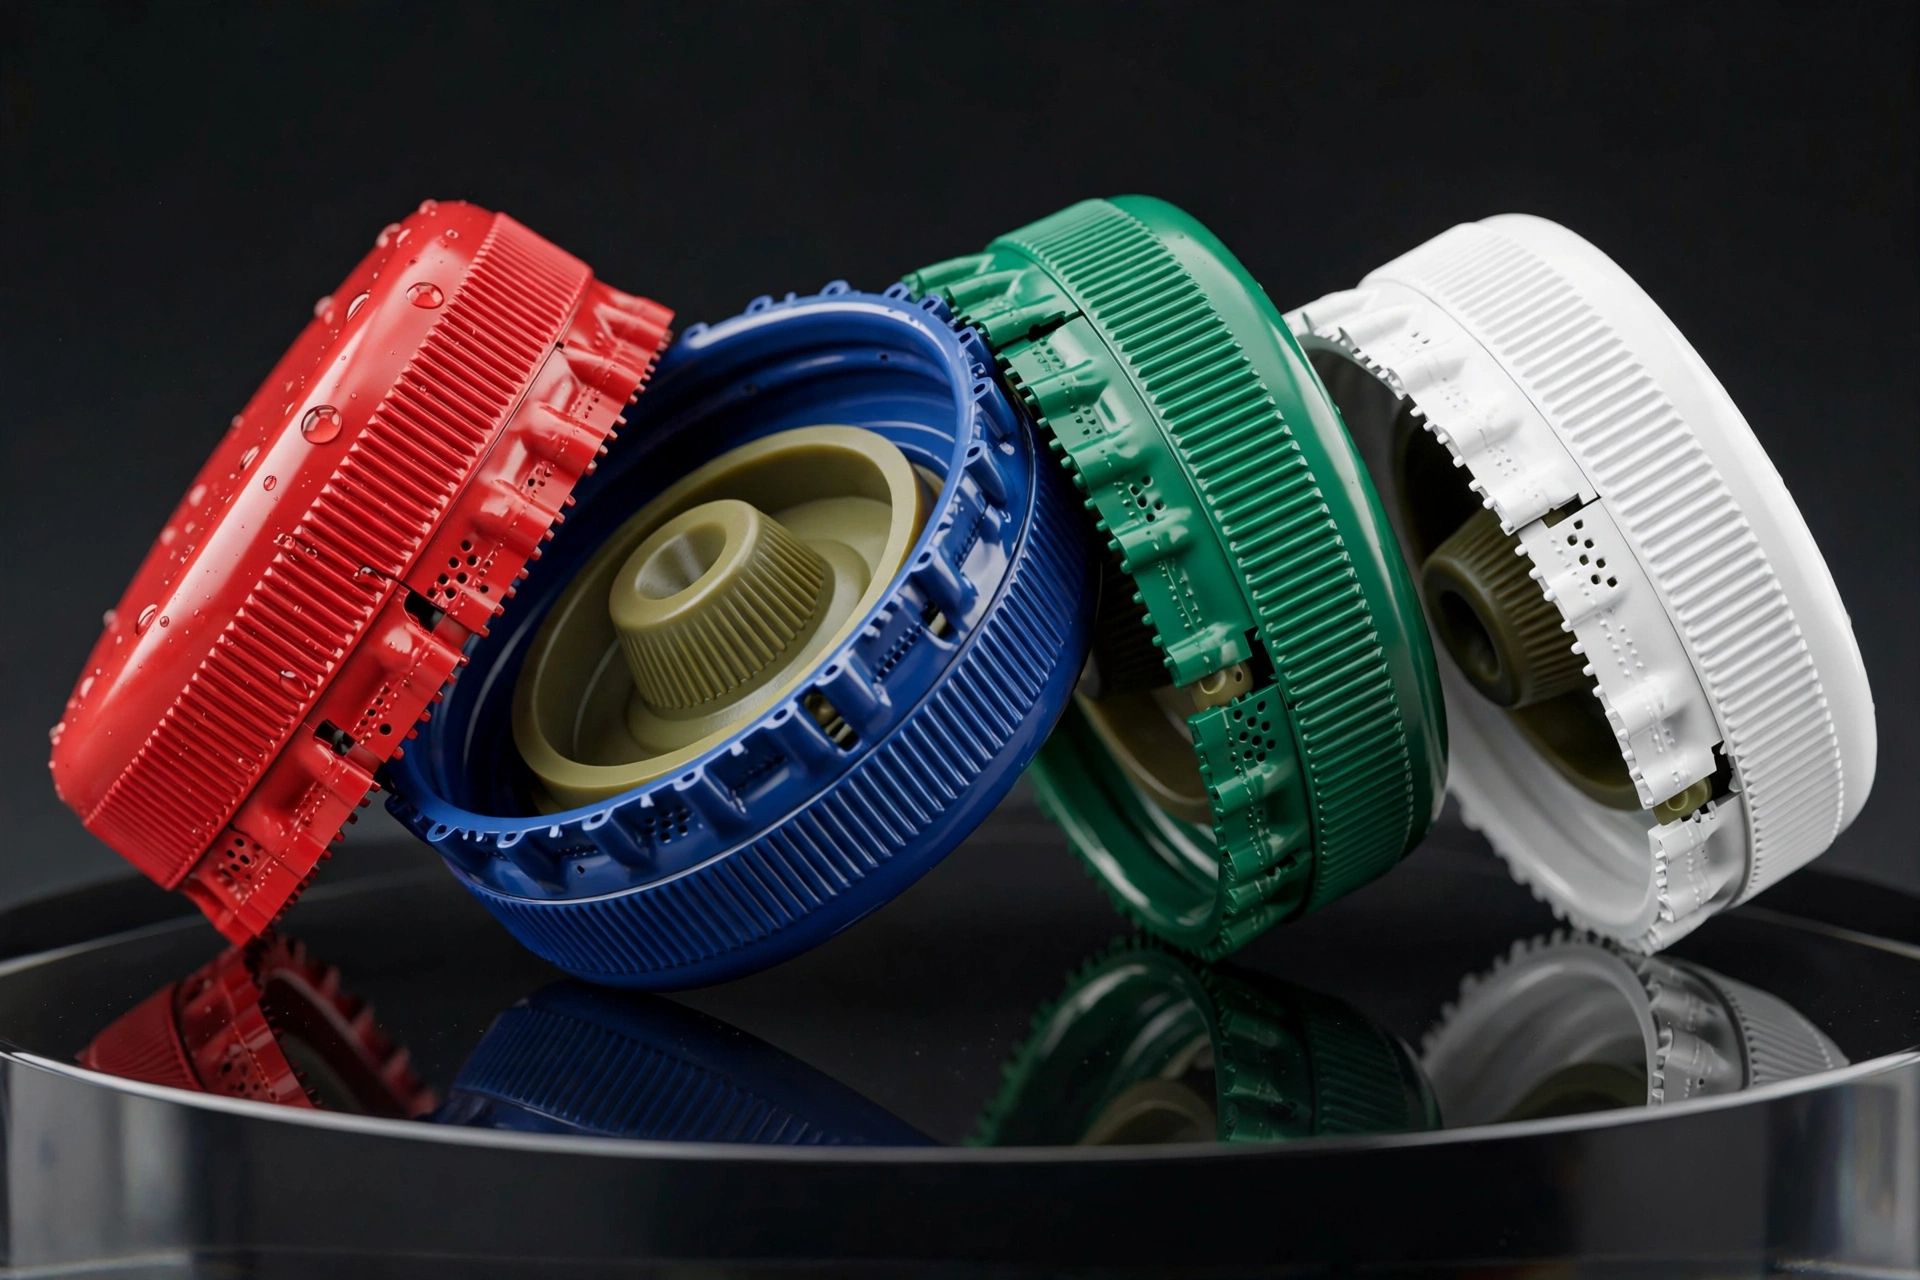
Interactive Closure Tooling Configurator
Select your cap architecture and annual production target to determine recommended cavitation, steel metallurgy, and demolding actuation.
Technical Sourcing FAQ: Packaging Tooling
Developing a High-Speed Packaging Closure Program?
Submit your cap drawings to Brandon Henderson in North Carolina. Receive full DFM review on living hinge geometry, unscrewing mechanisms, and high-cavitation hot runner layouts.