 Skip to content

Understanding Custom Injection Mold Tooling Architecture
Every injection molding program starts with the tool. Unlike a modular prototype base with hand load inserts, custom injection mold tooling is designed around one part: its resin and shrinkage, its cosmetic surfaces and undercuts, the cavitation needed to hit volume, and the press it will run in.
Primary Tooling Components
A production mold has to hold shut against the full clamp force of the press, from tens of tons on small medical parts to well over a thousand tons on large automotive tools, shot after shot. It is built from several precision machined subsystems:
- A Side (Cavity Half): The stationary half on the injection side of the press, usually forming the cosmetic outside of the part and carrying the sprue bushing or hot runner.
- B Side (Core Half): The moving half on the ejector side, forming internal ribs, bosses, snap fits and undercuts.
- Guided Ejection System: Ejector pins, blades, sleeves or stripper plates on a guided ejector plate that push the cooled part off the core without marking it.
- Slides and Lifters: Side actions driven by angle pins, cams or hydraulic cylinders that pull away from undercuts before the part ejects.

The stack from the top clamp plate down to the ejector housing: melt enters through the sprue bushing, cools against the water circuits, the mold opens at the parting line and the ejector system pushes the parts off the cores.
TK Group has built molds since 1983 and was ranked the No. 1 export toolmaker in China, with tooling capacity of more than 2,000 molds a year. That includes multi cavity and stack molds, insert molds and two and three shot molds for medical, packaging, automotive and consumer electronics customers.
Plastics Industry Association (SPI) Mold Classifications
The Plastics Industry Association (formerly SPI) classifies molds from Class 101 to Class 105 so buyers and toolmakers agree up front on expected tool life. Each class sets the expected number of cycles and the minimum construction that goes with it: steel hardness, mold base, guided ejection and cooling.
| SPI Class | Expected Life | Molding Surfaces | Mold Base | Typical Construction | Typical Applications |
|---|---|---|---|---|---|
| Class 101 | 1,000,000+ cycles | Hardened to 48 HRC minimum (for example S136, H13, 420 stainless) | Pre hardened, 28 HRC minimum | Guided ejection, hardened slide wear plates, plated or stainless water lines | Medical disposables, caps and closures, high volume packaging |
| Class 102 | Up to 1,000,000 cycles | Hardened to 48 HRC minimum | Pre hardened, 28 HRC minimum | Guided ejection recommended, hardened wear surfaces | Medium to high volume industrial and consumer parts |
| Class 103 | Under 500,000 cycles | 28 HRC minimum (P20, 718H or similar) | Standard steel | Standard drilled cooling | Medium volume appliance and power tool parts |
| Class 104 | Under 100,000 cycles | Mild steel, P20 or aluminum | Standard steel | Basic cooling | Low volume production |
| Class 105 | 500 cycles or fewer | Cast aluminum, epoxy or other soft material | Any | Prototype construction | Prototypes and fit checks |
For high volume programs, a Class 101 mold costs more up front but delivers the lowest cost per part over the life of the program, because hardened cavities, guided ejection and corrosion resistant cooling keep the tool running with less unplanned maintenance. For North American molders, see our export molds for U.S. presses, built to your press specs and component standards.

Tool Steel Metallurgy and Insert Hardening
Steel choice drives mold life, how well the cavity polishes, and how fast heat leaves the part. Match it to the resin: glass filled materials wear steel, PVC and some flame retardant grades attack it chemically, and optical parts need a steel that polishes to a mirror.
Key Tool Steels and Insert Alloys
- ASSAB S136 ESR (420 type stainless): Electro slag remelted stainless, typically hardened to about 48 to 52 HRC. Strong corrosion resistance for PVC, POM and flame retardant grades, and the go to steel for SPI A1 mirror polish and medical cavities.
- H13 (1.2344): Chromium molybdenum hot work steel hardened to about 48 to 52 HRC. Tough, resists heat checking, and holds up well to glass filled resins.
- NAK80: Pre hardened to about 40 HRC, so it is machined and polished without heat treat distortion. A good fit for detailed cavities and textured or high polish surfaces.
- High conductivity inserts: Copper alloys pull heat several times faster than tool steel. TK uses Moldmax HH beryllium copper core inserts to shorten cycle time, and beryllium free alloys such as Ampco 940 are an option where required.

| Steel or Alloy | Supplied As | Typical Working Hardness | Thermal Conductivity (approx.) | Polishability | Strengths |
|---|---|---|---|---|---|
| ASSAB S136 ESR | Annealed, about 215 HB | 48 to 52 HRC, hardened | 16 W/(m·K) | SPI A1 (mirror) | Corrosion resistance, polish, wear life |
| H13 (1.2344) | Annealed, about 220 HB | 48 to 52 HRC, hardened | 25 W/(m·K) | SPI A2 | Toughness, thermal fatigue resistance |
| NAK80 | Pre hardened, about 40 HRC | About 40 HRC, no heat treat | 41 W/(m·K) | SPI A1 to A2 | No heat treat distortion, machinability |
| P20+Ni (1.2738) | Pre hardened, 28 to 34 HRC | 28 to 34 HRC, nitriding optional | 33 W/(m·K) | SPI B1 to B2 | Economical for Class 103 and 104 tools |
| Ampco 940 | Finished bar | About 94 HRB | 208 W/(m·K) | Functional | Very high heat transfer, beryllium free |
Values are typical figures from steel maker data sheets and vary by supplier and heat treatment. TK confirms the grade and hardness for each insert on the steel certificate and heat treat report.
Gating Architecture and Mold Thermal Management
Cooling is usually the longest part of the molding cycle, often more than half of it. If heat leaves the core and cavity unevenly, the part warps, sinks and needs a longer cycle to hold size. Balanced gating and well placed cooling circuits are where most cycle time is won or lost.

Conformal Cooling vs Conventional Drilled Circuits
Straight drilled water lines can only go where a drill can reach, which leaves deep cores and tall ribs running hot. Conformal cooling inserts are 3D printed with channels that follow the part shape, so heat leaves evenly.
TK prints conformal inserts in house on a 3D Systems DMP 350 in 1.2709 maraging steel, aged to 50 to 56 HRC. TK has seen cycle time reductions of up to 35%, and a conformal cooled critical insert cut the cycle by 22% on a 12+12 cavity two shot flip top cap mold. Learn more on our conformal cooling page or see our high cavitation and stack molds.
Step-by-Step Custom Mold Development Workflow
Turning a 3D CAD model into a qualified production mold follows a gated process, so problems get caught in design review instead of in hardened steel. A typical TK build takes 3 to 6 months, compared with 8 to 18 months at many EU and U.S. toolmakers, and documented programs have shipped in as little as 10 weeks from purchase order.
- 1Kick OffPart, resin, volume and press review
- 2DFM and MoldflowGate, wall, draft and warpage review
- 3Mold DesignFull 3D design and checking, customer approval
- 4FabricationCNC, EDM, grinding with in process QC
- 5Trial and VerifyScientific mold test, CMM sample report
- 6OptimizeECRs and fine tuning to approval
- 7Delivery and LaunchShipment, on site start up support, SOP
1. DFM and Moldflow Review
Before steel is cut, TK’s Moldflow analysts (certified at Gold, Silver and Bronze level) run fill, cooling and warpage analysis to find weld lines, air traps and shrinkage problems, and design the mold in UG NX. See our DFM and Moldflow services.
2. Micron Level CNC and EDM
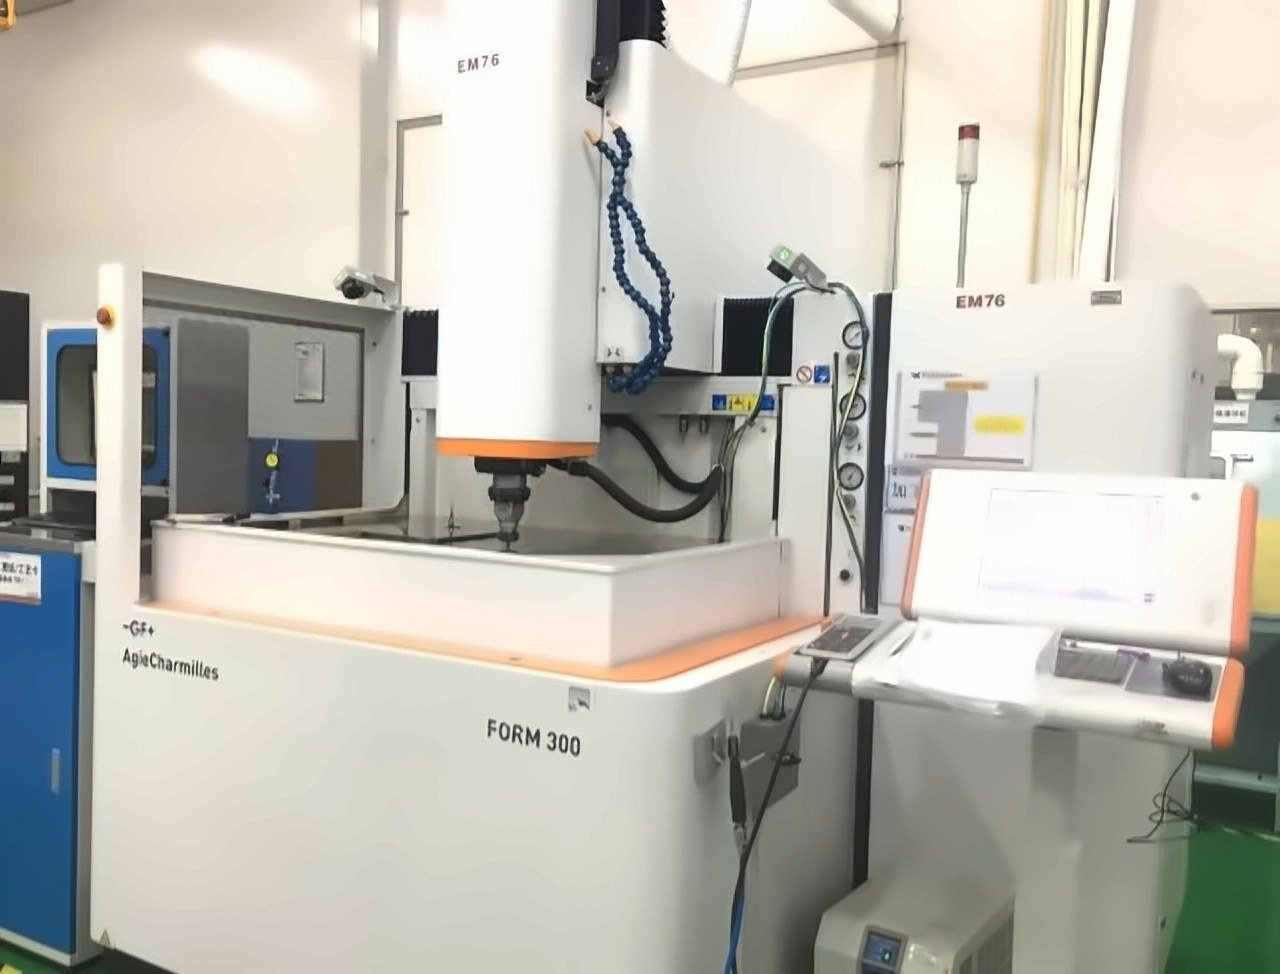
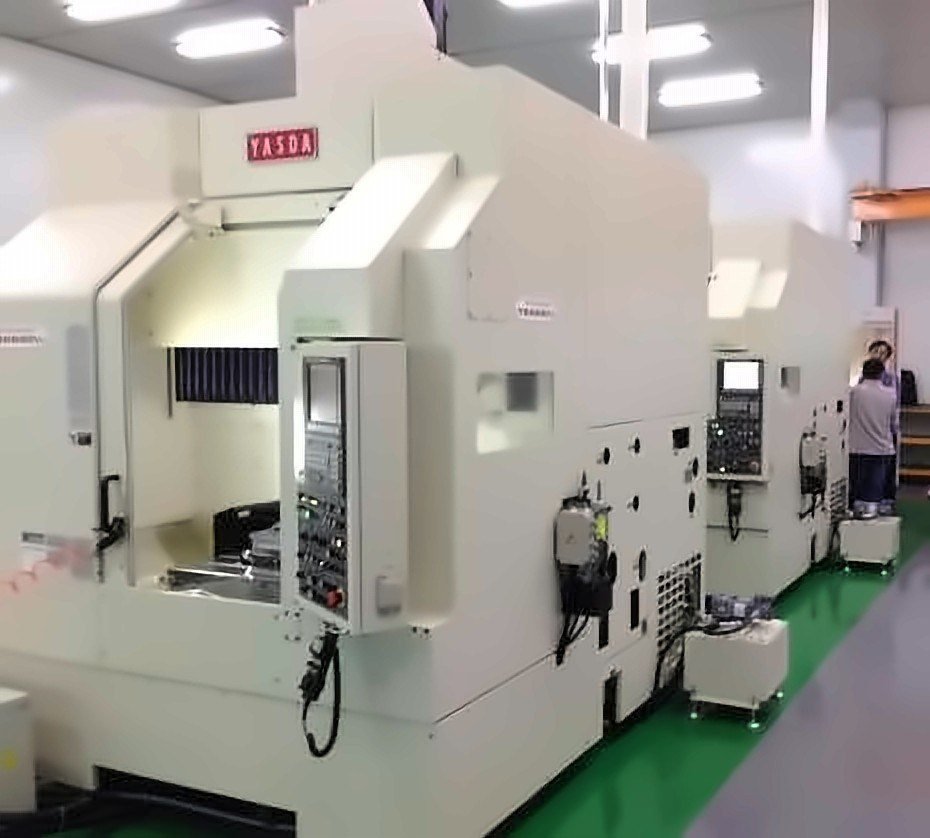
Inserts are machined on Röders, Yasda and Makino high speed machining centers, burned and wire cut on Agie Charmilles EDM, and ground on Studer and Hauser jig grinding equipment, holding molding insert tolerances to 0.002 mm.
3. Scientific T1 Mold Trial
Every mold is trialed in house on presses from 50 to 1,500 tons using scientific mold testing: short shot balance, pressure loss, cooling circuit and mold temperature checks, and optimized hold pressure and time, with CMM inspection of the samples. See our mold trials.

Custom Tooling Specifier and Cavity Estimator
Enter your annual volume, expected cycle time and part size. The calculator works out the minimum cavity count your press time can support, a balanced cavity layout, the SPI class your lifetime shots call for, a clamp tonnage range, and a starting steel and runner recommendation. Open “Show the math” to see every number worked out.
Show the math
A starting point for quoting, not a final design. Cavity count is exact for the numbers you enter. Tonnage uses common rule of thumb clamp factors by resin; TK confirms the real number with Moldflow. Final steel, runner and cavitation are set in DFM.
Coordinate Metrology, First Article Inspection (FAI), and CMM Verification
Holding size across every cavity of a multi cavity tool takes measurement at every stage: incoming steel, machined inserts, the assembled mold and the molded samples. TK checks steel hardness and chemistry on arrival, inspects machined inserts in process, and measures trial samples on CMM before a mold ships.
Dimensional Verification at TK
- Coordinate Measuring Machines (CMM): A fleet of 17 to 20 CMMs, including Zeiss, for inserts, electrodes and molded samples.
- Optical Measurement: Vision measuring machines and OGP optical systems for small features and thin walls that a touch probe can deflect.
- CT Scanning: Industrial CT in the lab to see inside a part without cutting it: wall thickness, voids and core shift.
- Capability Studies: CPK above 1.67 on 200+ control dimensions on precision programs, and 100% CMM inspection with a 99.8% or better pass rate on critical dimensions.
- Steel Verification: Spectral analysis and hardness testing of incoming steel, with heat treat reports kept for every insert.

For programs that move straight into production, see our contract injection molding services, or our multi shot injection molding capabilities for two color and soft touch overmolding.
Technical Inquiries About Custom Injection Mold Tooling
Direct answers to the questions engineers and buyers ask most when choosing a tooling partner.
Ready to Review Your Part Geometry for Custom Tooling?
Connect directly with Brandon Henderson, Journeyman Tool and Die Maker (CPSP) based in North Carolina. Receive an initial Design for Manufacturability (DFM) review and tooling quotation within 24 to 48 hours.