
Advanced Injection Press Fleet: 6T to 1,500T
Successful contract manufacturing requires having the exact machine size, screw geometry, and clamping technology required for the part design. Running a thin-walled medical cartridge on an oversized hydraulic machine consumes excessive energy and creates thermal degradation, while running a structural housing on an under-tonnage press causes parting line flash.
Fleet Composition & Technology
Our manufacturing operations encompass five hundred and three injection molding machines located across four specialized campuses:
- 355 Horizontal Presses: General commercial, consumer electronics, packaging, and industrial production lines.
- 60 Multi-Shot (2K/3K) Machines: Integrated rotary tables and secondary injection barrels for chemical bonding of two and three materials.
- 40 Vertical Insert Machines: Dedicated to insert molding over pre-stamped brass terminals, threaded bushings, and micro-electronic PCBs.
- 25 High-Speed Thin-Wall Presses: High-acceleration machines with injection speeds up to 800 mm/sec for packaging closures.
- 20 Liquid Silicone Rubber (LSR) Presses: Chilled runner, precision-metering pumps for medical diaphragms and automotive seals.
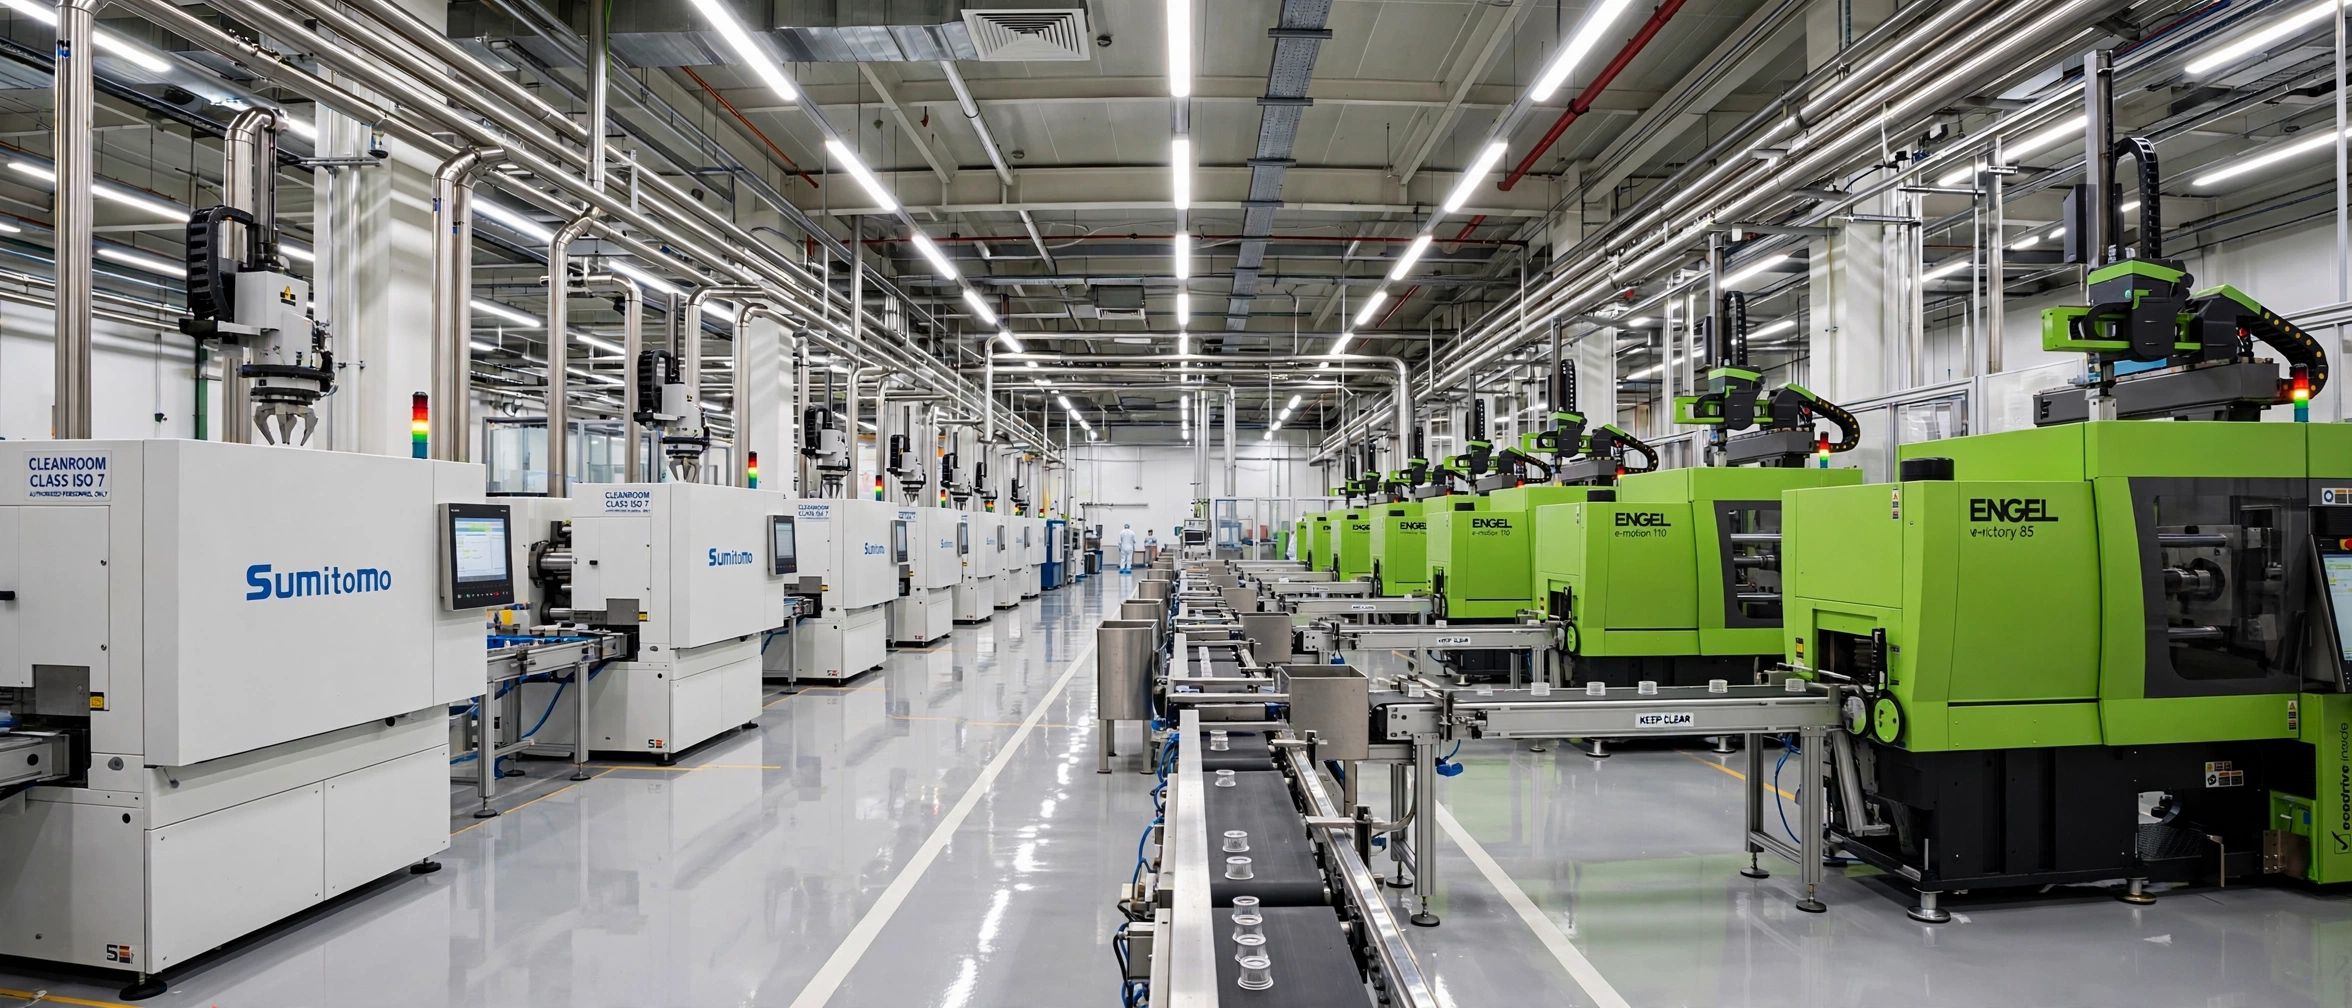
In research documented by the National Institute of Standards and Technology on manufacturing sustainability, electric servo presses demonstrate up to fifty percent energy savings while delivering shot-to-shot consistency within 0.05 percent volumetric variation.
Class 100,000 Cleanroom Medical Molding
For medical diagnostics, microfluidics, and drug delivery devices, manufacturing environments must eliminate airborne particulates, bioburden contamination, and human contact. Our cleanroom facilities are certified under ISO 13485 and operated in full compliance with current Good Manufacturing Practice (cGMP) standards.
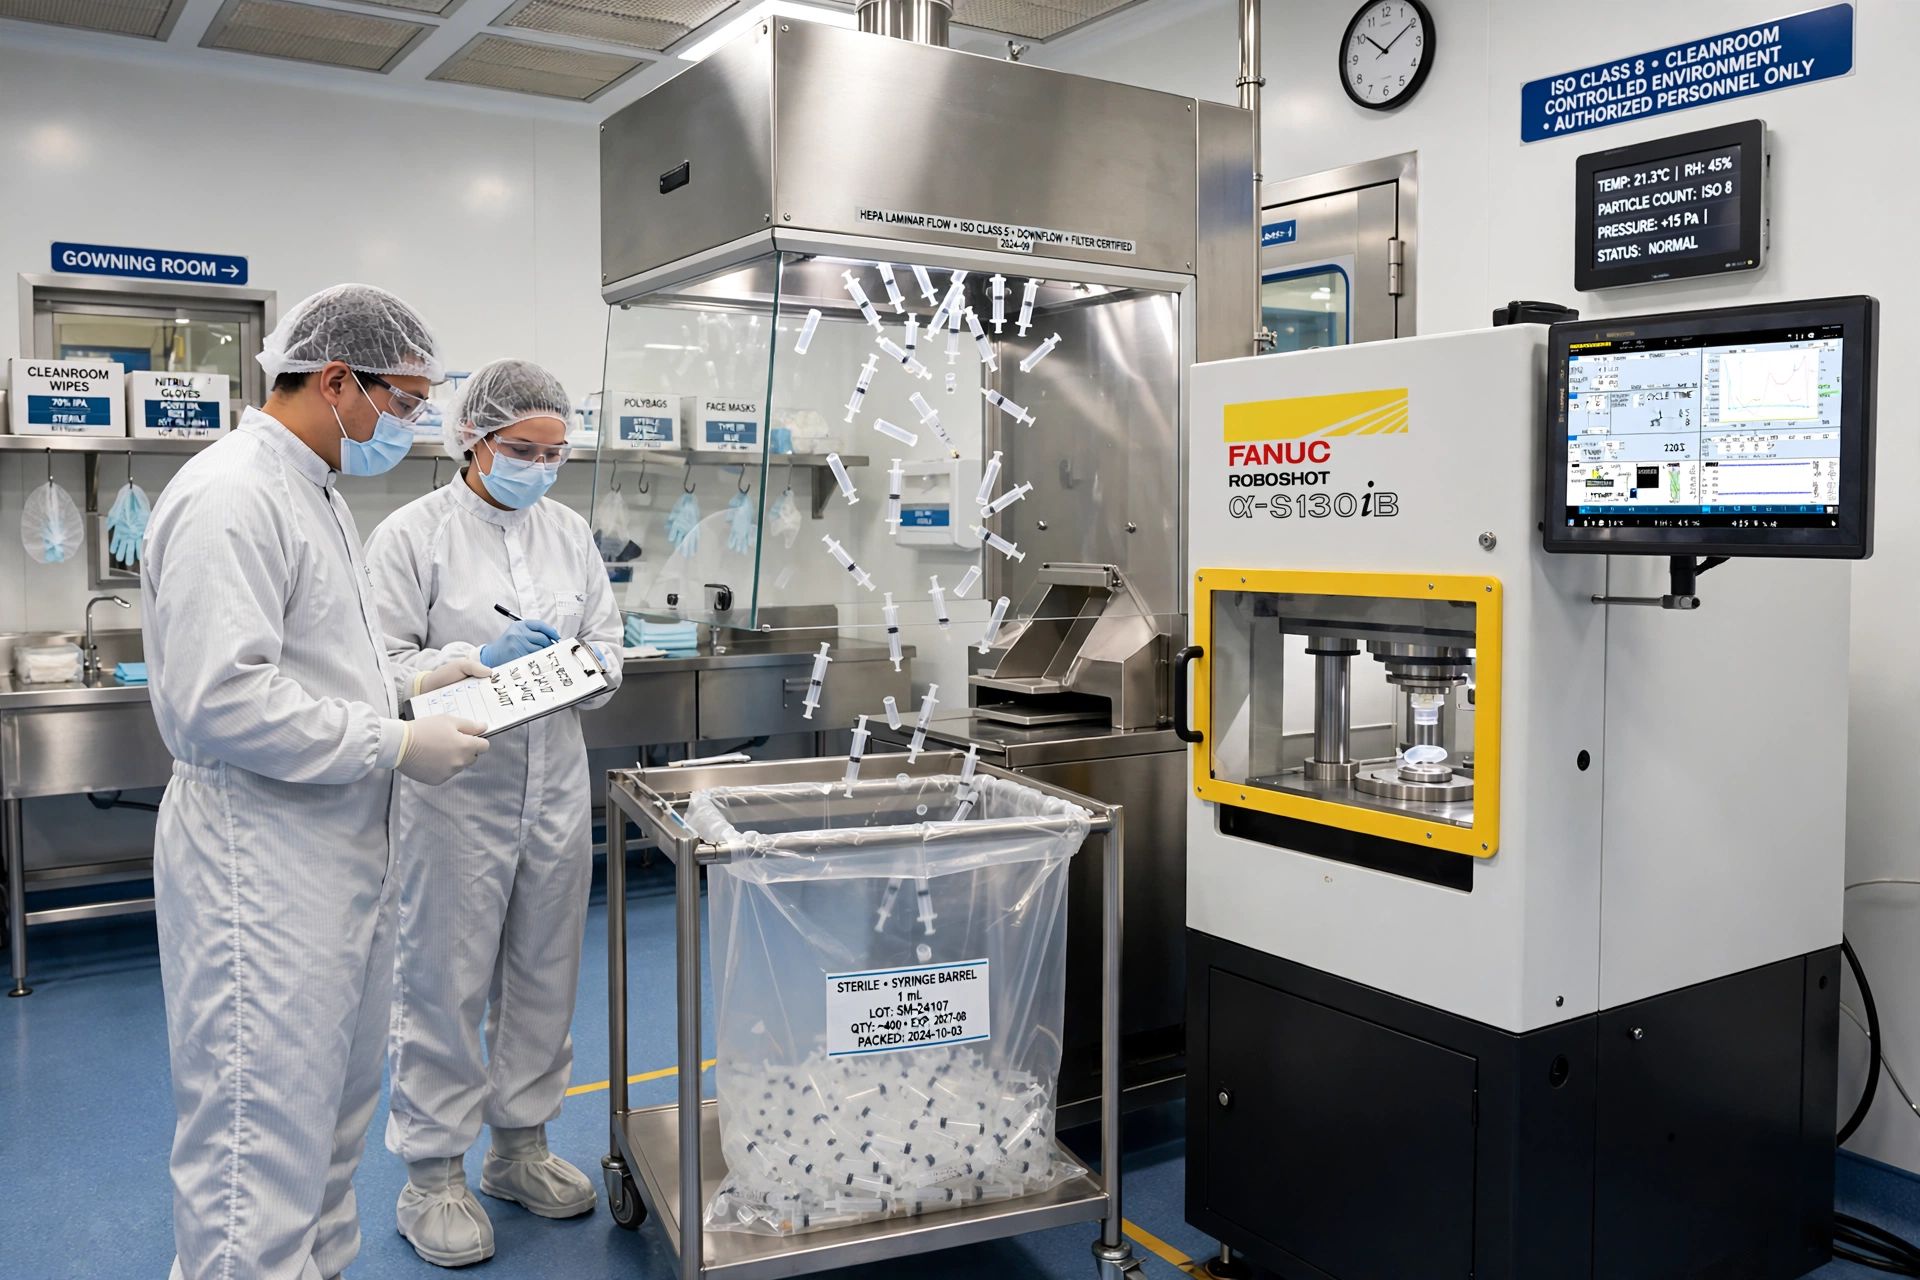
Medical Manufacturing Protocols
Our medical business division provides comprehensive product validation protocols:
- Installation Qualification (IQ): Verification of machine calibration, utility hookups, and instrumentation accuracy.
- Operational Qualification (OQ): Defining robust process parameter windows using design of experiments (DOE).
- Performance Qualification (PQ): Demonstrating long-term statistical process stability across three consecutive production shifts.
- 100% Optical Inspection: High-speed vision inspection detecting micro-particulate contamination and flash.
High-Performance Engineering Resin Expertise
Processing specialized polymers requires precise melt temperature regulation, pressurized mold heating, and corrosion-resistant barrels. We process more than seven thousand tons of thermoplastic resin annually, including demanding high-temperature formulations.
| Polymer Family | Common Trade Grades | Molding Temp (°C) | Mold Temp (°C) | Key Performance Strengths |
|---|---|---|---|---|
| PEEK / PEKK | Victrex 450G, KetaSpire | 370 – 400°C | 160 – 200°C (Oil Heated) | Extreme temperature resistance; chemical inertness |
| PPS (Polyphenylene Sulfide) | Ryton, Fortron | 310 – 350°C | 130 – 150°C | Dimensional stability; flame retardant; automotive fluids |
| Polycarbonate (PC) | Lexan, Makrolon | 280 – 320°C | 80 – 110°C | Optical clarity; high impact strength |
| PA66-GF50 (50% Glass Nylon) | Zytel, Durethan | 285 – 305°C | 90 – 120°C | High structural rigidity; metal replacement |
| Liquid Silicone (LSR) | Silopren, Elastosil | 15 – 25°C (Chilled Barrel) | 170 – 210°C (Heated Mold) | Biocompatible; flexible down to -50°C |
Multi-Shot (2K/3K) Chemical Bonding
Combining a rigid engineering substrate with a soft-touch elastomeric seal in a single automated molding cycle eliminates manual assembly, leaks, and adhesive bonding. Learn more on our dedicated multi-shot injection molding page.
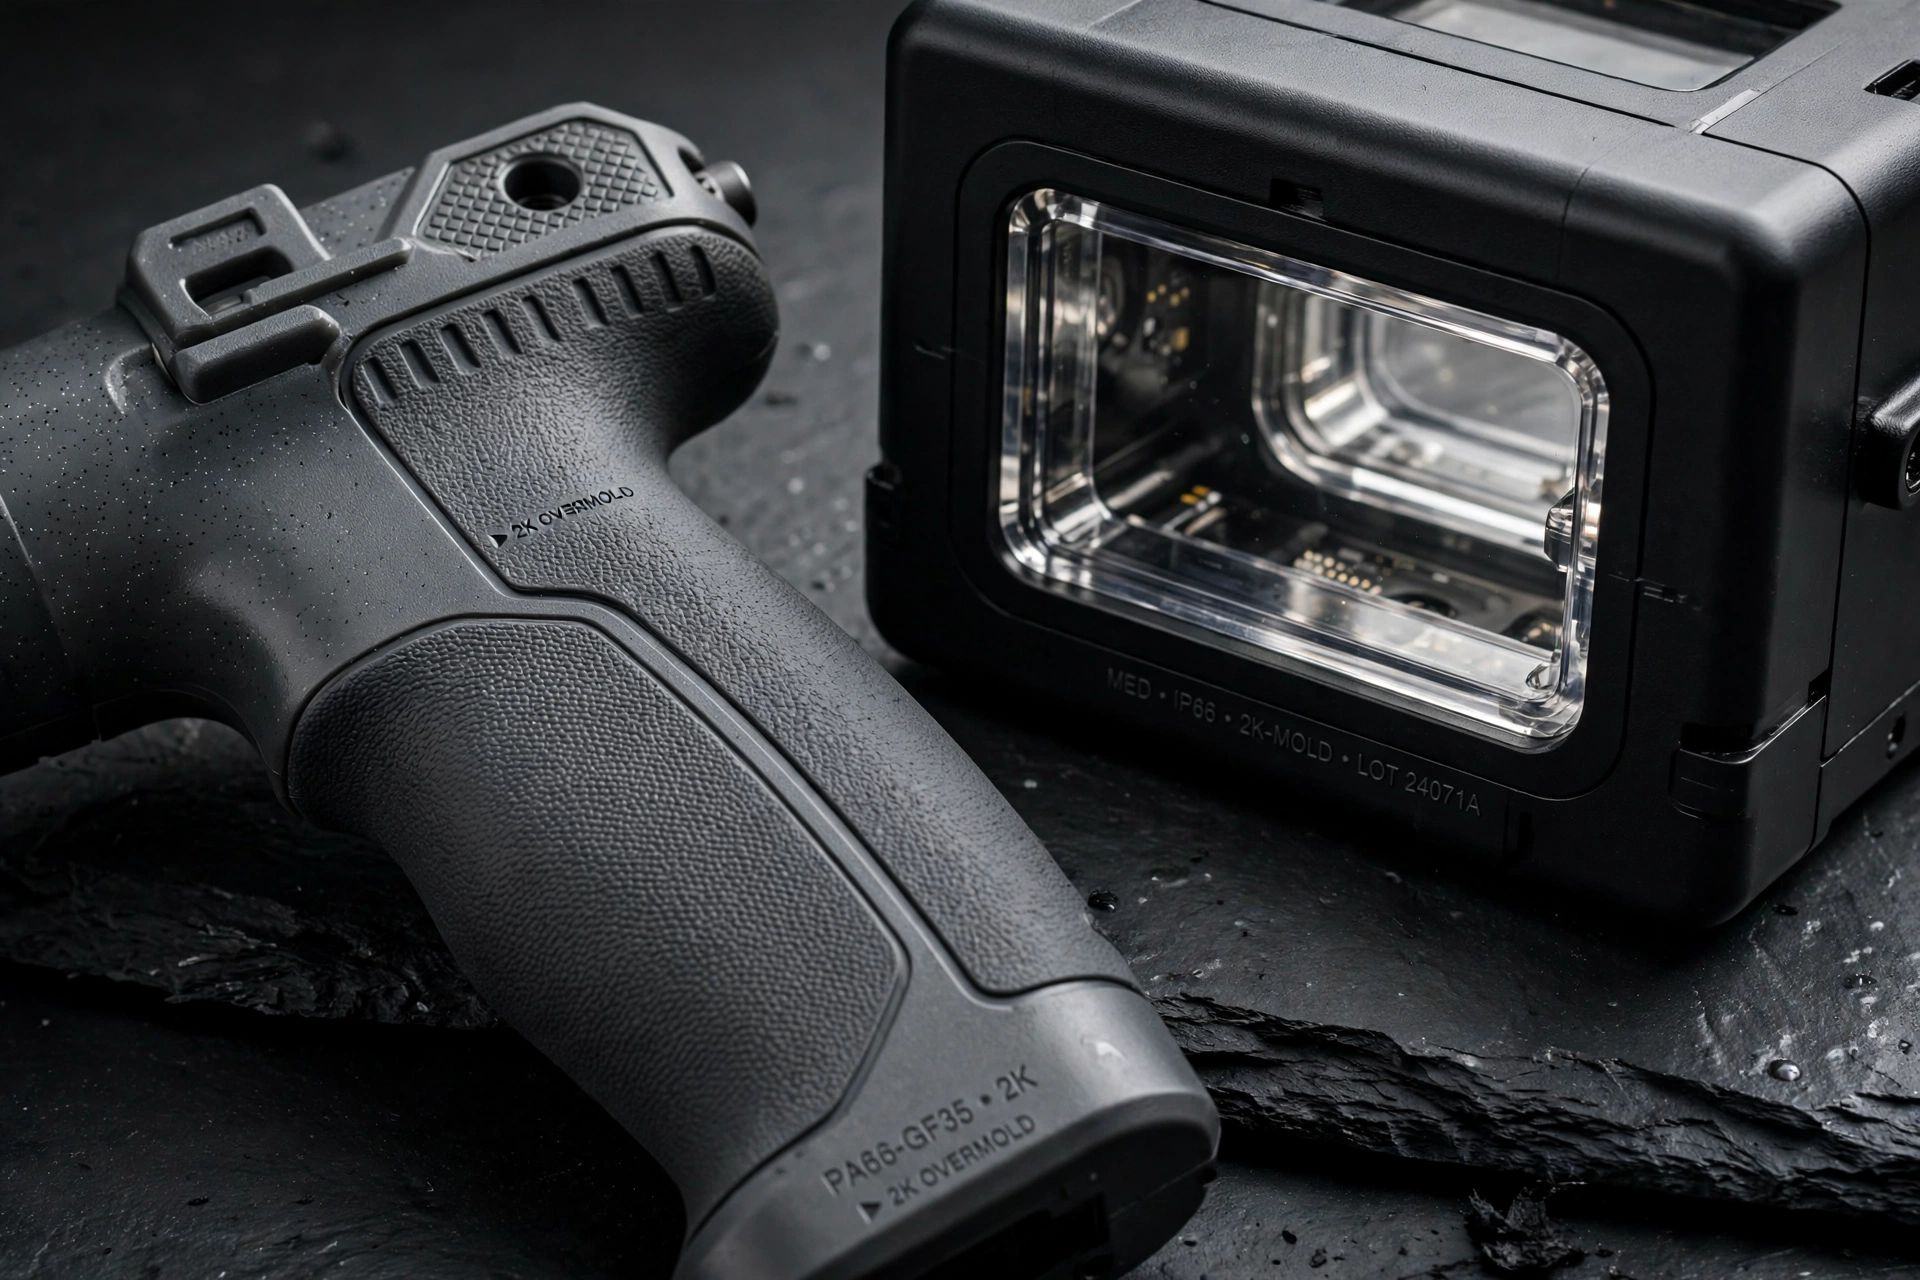
Automated Robotic Handling and Degating
Every high-volume cell is fitted with customized End-of-Arm Tooling (EOAT). Pneumatic and vacuum grippers extract parts without touching cosmetic class-A surfaces, separating cold runners directly onto granulator conveyors for closed-loop sprueless production.
Secondary Decoration, Coating, and Final Assembly
Delivering turnkey finished products requires seamless secondary processing without logistical freight handoffs between multiple contract vendors.
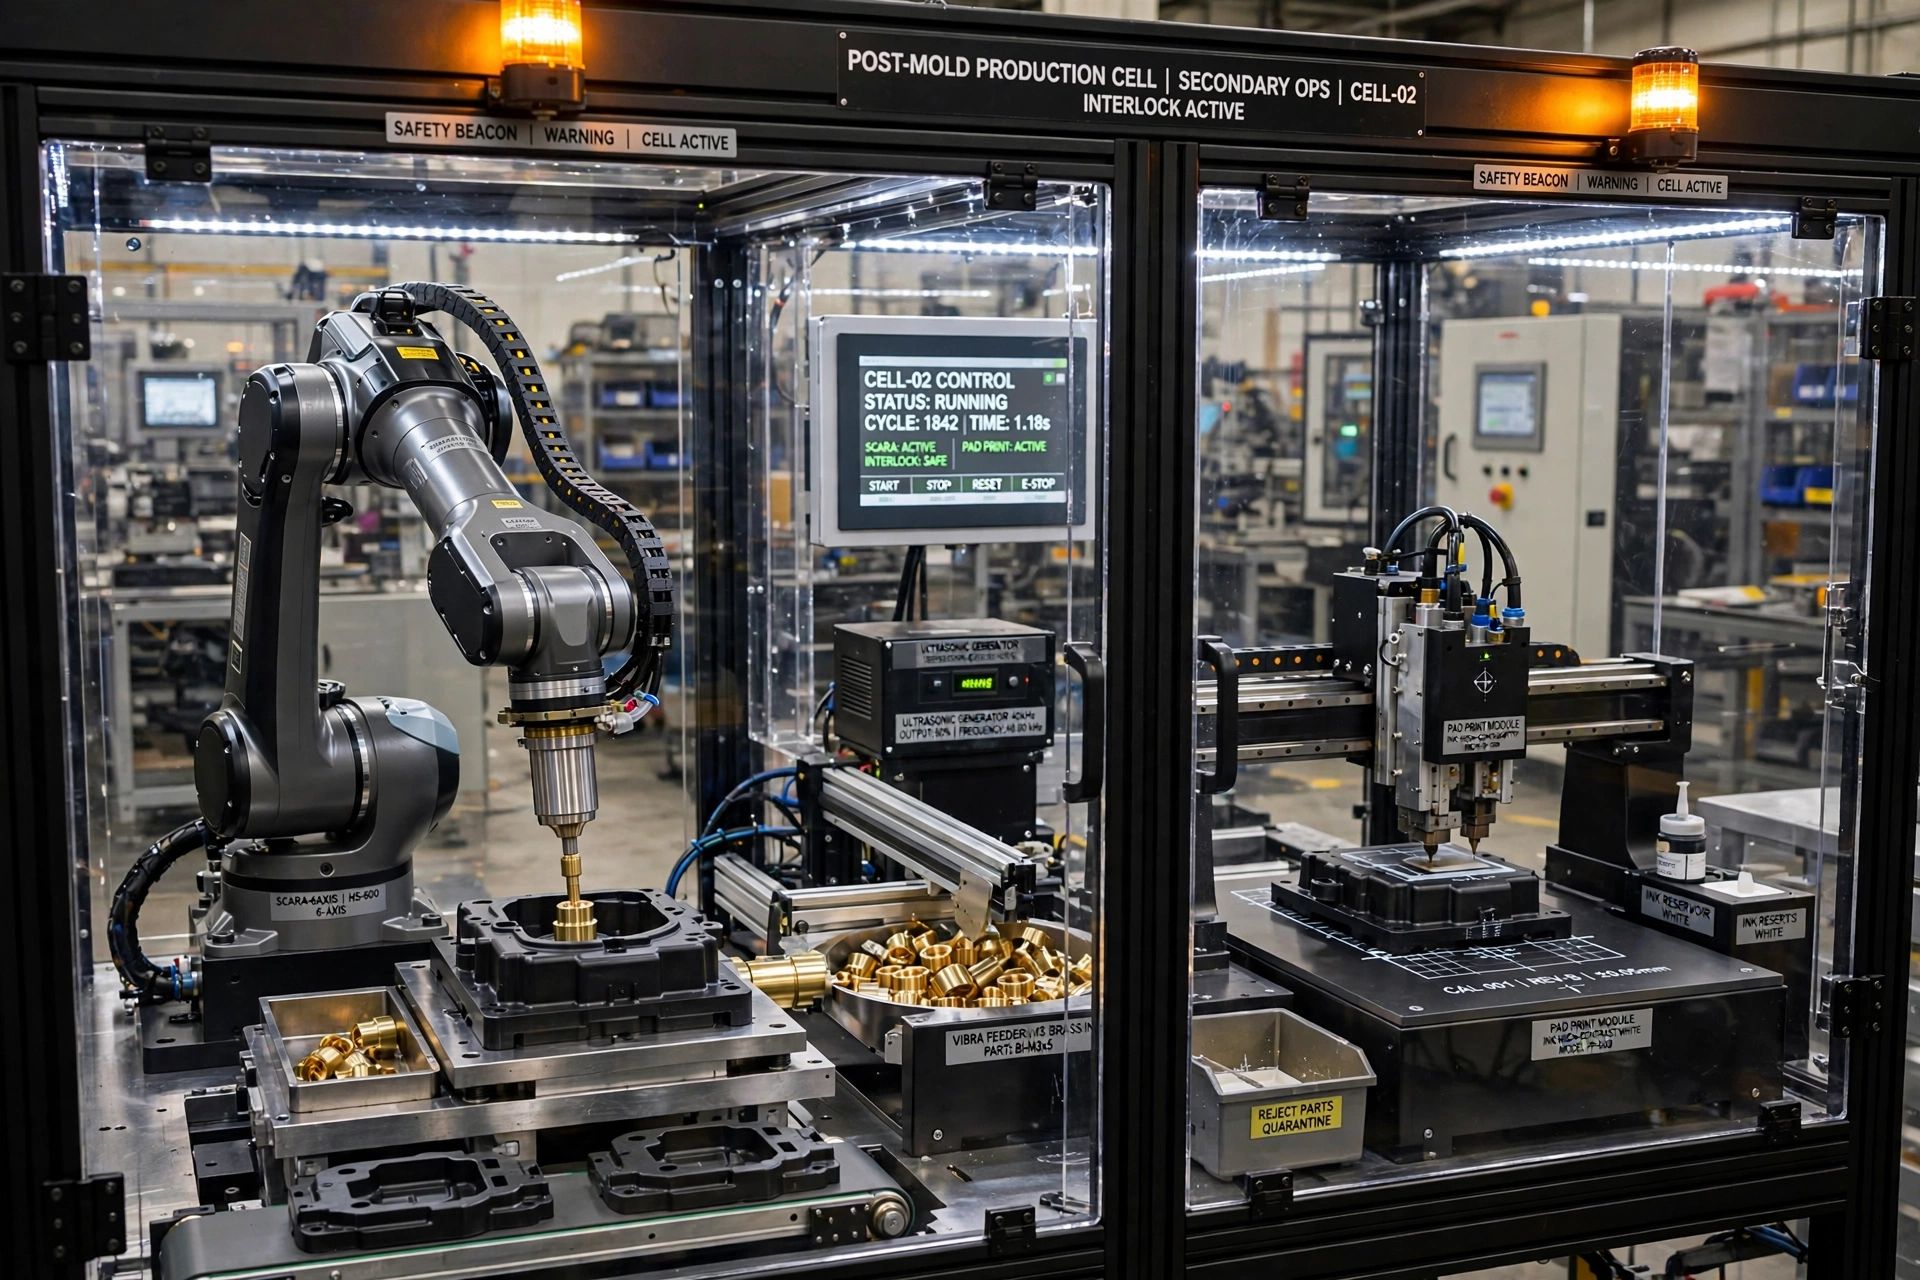
In-House Secondary Operations
- Automated Spray Painting: Four robotic spindle painting lines ranging from 450 to 560 meters in length, operating inside Class 10k spray booths.
- Non-Conductive Vacuum Metallization (NCVM): Delivers chrome and brushed metallic aesthetics that do not interfere with 5G or RF wireless antennas.
- Printing and Laser Engraving: Pad printing, 6-color silkscreening, high-speed offset printing, and precision laser etching.
- Ultrasonic and Heat Stake Assembly: Automated assembly inserting threaded brass inserts and welding multi-component housings.
Interactive Press Tonnage Estimator
Estimate the required clamping tonnage for your injection molded component by entering part dimensions and projected cavitation.
Technical Sourcing FAQ: Contract Injection Molding
Looking for a Scalable Contract Molding Partner?
Discuss your piece-part volume forecasts and cleanroom specifications with Brandon Henderson, our North Carolina technical broker. Receive detailed part costing, mold build timelines, and resin optimization recommendations.