We prove tooling performance on the factory floor before steel ever leaves Asia. Click any video below to inspect real-world cycle times, mechanical actions, and part ejections.
HIGH-DEFINITION TRIAL FOOTAGE
Tested Under True Production Conditions
Every mold is trial-shot using your specified production resin and color masterbatch on properly sized electric or servo-hydraulic injection presses.
Stack Tooling • 96 Cavities Total
48+48 Flip-Top Stack Mold
8.5s cycle time • S136 ESR Hardened (52 HRC) • Synchronized in-mold closing rack mechanism • Mold-Masters 96-drop hot runner
High Cavitation Packaging
72-Cavity Flip-Top Mold
7.2s cycle time • Single-face high-speed cap tool • Husky 72-drop balanced hot runner • Conformal cooling cores
Dual living hinge spice cap • Stripper plate bump-off undercut ejection • H13 TiN coated inserts • High cavitation
Corporate Facility Tour
TK Group Smart Factory Tour
Walk through our 200,000 m² smart campuses • 325 CNC/EDM toolmaking centers • Automated robotic AGVs • Class 100k cleanrooms
Toolmaking Operations
High-Speed Tooling Bays
High-speed 5-axis milling, submerged Sodick wire EDM cutting, and robotic die sinker EDM electrode management
QUALITY PROTOCOLS
Brandon Henderson's 6-Step T1 Validation Protocol
How a Journeyman Toolmaker guarantees that every export mold arrives production-ready at your US molding facility.
01
4-Hour Continuous Dry Cycle
The mold is mounted in a press and cycled dry continuously for 4 hours to verify mechanical slider timing, lifter clearance, guide pin alignment, and hydraulic sequence switches under thermal equilibrium.
02
Scientific Molding Window Study
Using RJG eDART cavity pressure sensors and decoupled molding principles, we establish a robust viscosity curve and process window, ensuring the mold is forgiving across resin lot variances.
03
32-Point CMM Inspection Report
Samples from every single cavity are measured on Zeiss multi-sensor CMMs and Keyence optical comparators against your 2D print tolerances. Complete CPK capability studies are documented.
04
Steel-Safe Tool Adjustments
Critical shutoffs, draft angles, and tight press-fit dimensions are purposely machined steel-safe. Brandon reviews T1 dimensions and authorizes final micro-EDM or polishing passes to hit nominal.
05
Air-Freight of Physical T1 Parts
Physical molded parts are air-freighted via DHL/FedEx directly to Brandon in North Carolina and your engineering department for hands-on fit-and-function testing and official sign-off.
06
Export Crating & DDP Shipment
Once signed off, water lines are purged and blown dry, cores and cavities treated with heavy-duty anti-rust oil, safety latches installed, and packed in reinforced export crates with full CAD and steel certs.
Direct American Accountability
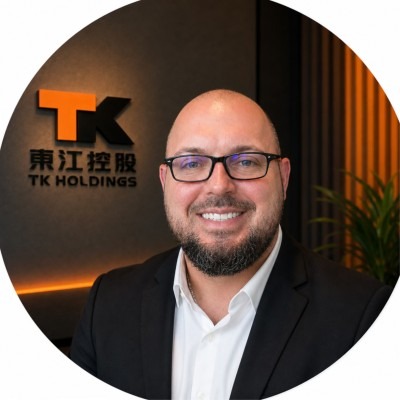
Brandon Henderson Personally Inspects Every T1 Part
“I don’t clear an export mold for crating until physical molded parts sit in my hands here in North Carolina, dimensional CMM layouts match your print, and cycle times meet production requirements.”